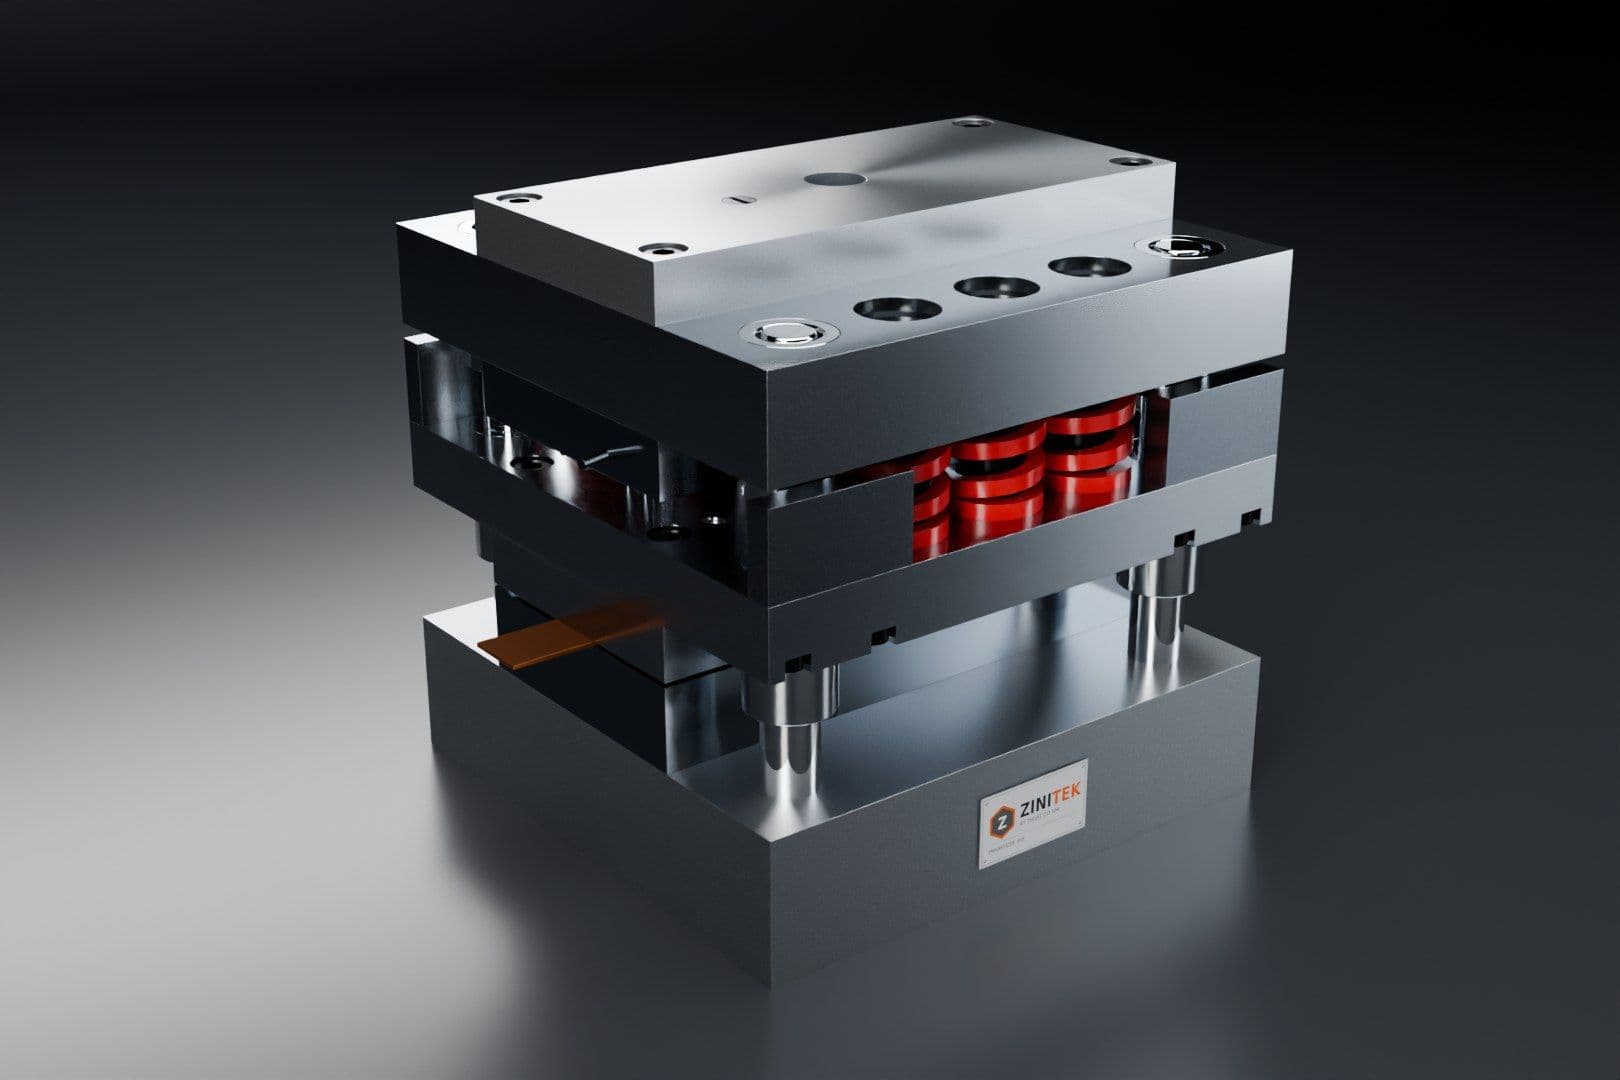
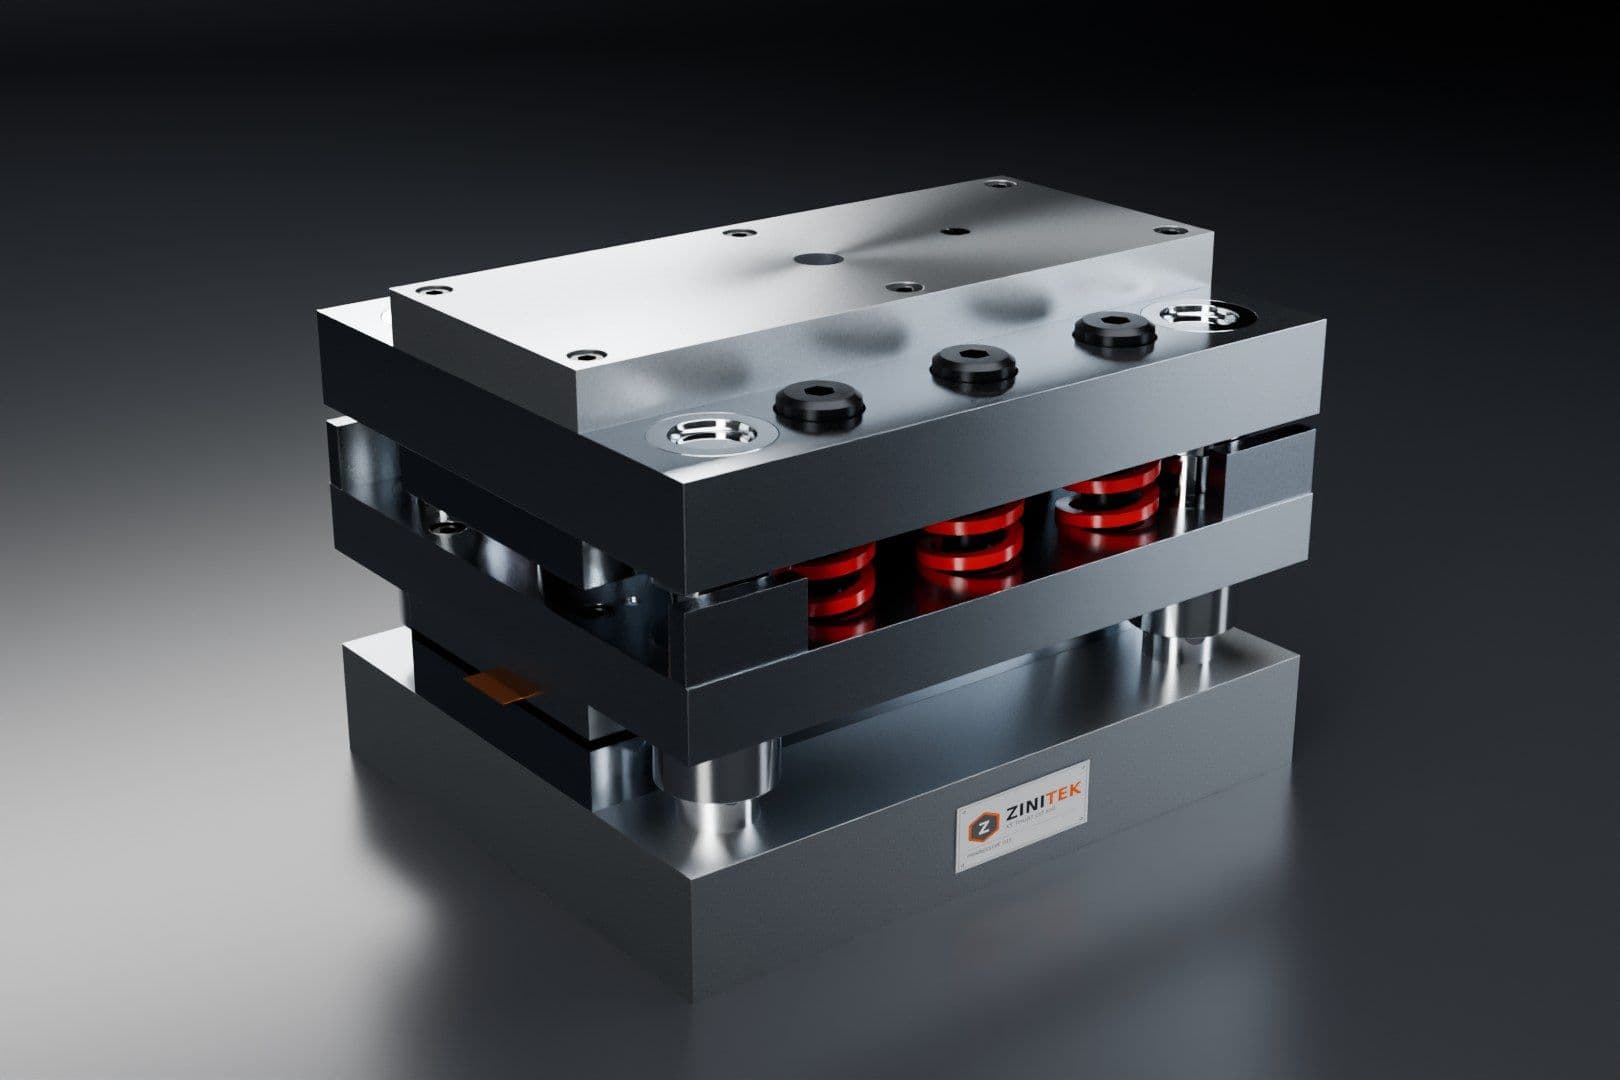
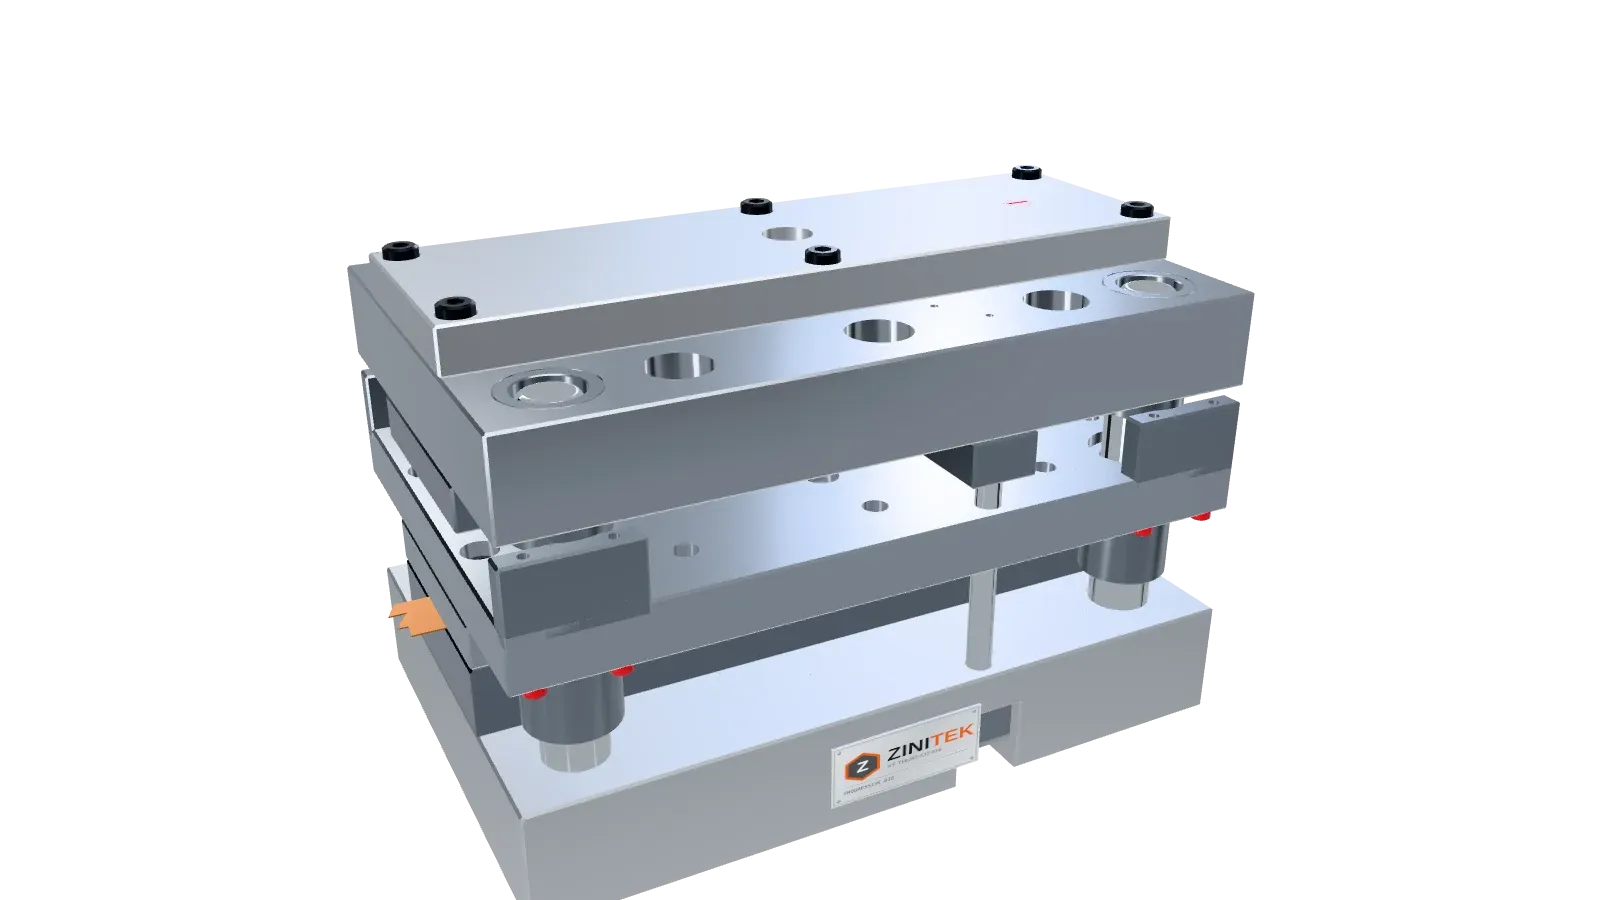
Progressive Die for 10A Electrical Contacts: 27 mm strip, 15.5 mm pitch. Ø2 and Ø3.5 piercing, contour cutting, 30° and 90° bending over several bending punches, with a pitch-check device and lever. Rotate the animated 3D model right on this page.
Ø2 and Ø3.5 piercing, contour cutting, 30° and 90° bending over several bending punches, with a pitch-check device and lever; Ø2/Ø3.5 pilots locate the copper strip.
27 mm wide strip with a 15.5 mm pitch. The animated 3D model shows the die opening and closing and the strip advancing one pitch per cycle.
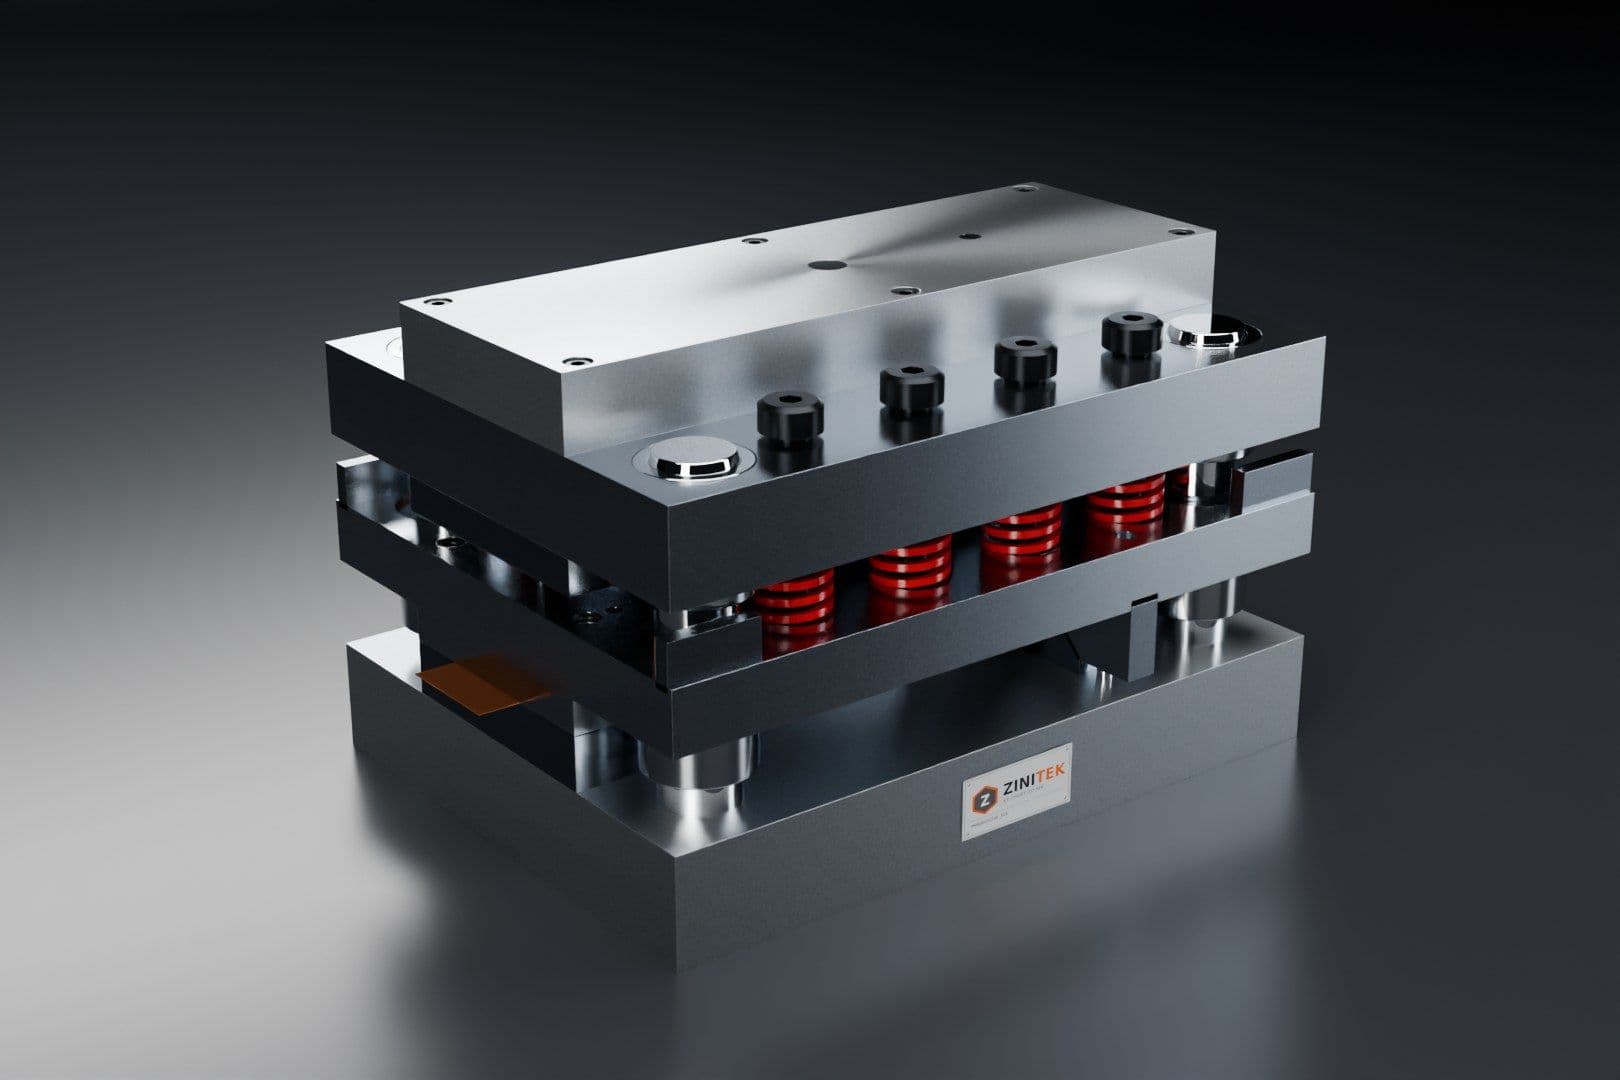
A spring stripper clamps the strip flat before the punches cut and strips it off the punches as the die opens; the springs compress with the stripper travel.
Guided by 4 pillars and bushes; a press stroke of about 30 mm keeps the pillars engaged in their bushes throughout the cycle.
Cutting and forming parts in SKD11 tool steel hardened to 58–62 HRC; shoes and holder plates in S50C to keep cost down; standard screws, dowels, pillars, bushes and springs.
Order to your drawing: send the part drawing, material and thickness, volume and press data, and ZINITEK will propose the strip layout and die design.
 Precision Mold Design & Manufacturing